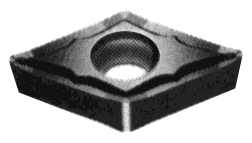

Coating technology is where most of the real productivity in steel machining has been won over the past two decades. Among the systems that reset expectations for PVD-coated carbide, Kyocera MEGACOAT NANO stands out: a nano-layer coating architecture that pushed hardness, oxidation resistance and edge toughness well beyond conventional monolayer TiAlN. This guide explains how the technology works, which grades use it, how it compares with competing coatings, and which starting parameters to use when machining steel.
What Is MEGACOAT NANO?
MEGACOAT NANO is Kyocera’s proprietary nano-layer PVD coating family, built primarily on aluminium-rich AlTiN compounds. Where a conventional PVD coating deposits a handful of layers, each measured in microns, MEGACOAT NANO alternates many extremely thin sub-layers whose individual thickness is measured in nanometers, while total coating thickness stays in the familiar PVD range of roughly 1.5 to 4 µm depending on grade and application.
The practical consequences for steel cutting are significant:
- Higher hardness. The nano-refined grain structure supports hardness in the region of approximately 3,300-3,600 HV, compared with roughly 2,800-3,200 HV for typical monolayer TiAlN.
- Higher hot hardness and oxidation resistance. Aluminium-rich chemistry forms protective alumina at temperature, with useful oxidation resistance up to approximately 1,100 °C.
- Better edge toughness. Layer interfaces arrest and deflect micro-cracks, reducing edge chipping in interrupted cuts.
- Smoother as-deposited surface. Fine, dense grains reduce surface roughness, lowering friction and the tendency to built-up edge on gummy low-carbon steels.
These properties matter because steel machining, for all its familiarity, stresses a cutting edge in four different ways at once: abrasion, adhesion, diffusion and thermal cycling. A coating that only wins on hardness loses on one of the other three. The nano-layer approach was engineered to move all four needle gauges simultaneously.
The Science Behind Nano-Layer PVD Coatings
In a monolayer TiAlN coating, a crack initiated by mechanical or thermal shock can propagate relatively freely through the coating until it reaches the carbide substrate, where it concentrates stress at the cutting edge and eventually produces chipping. In a nano-layer coating, every interface between chemically or structurally different sub-layers forces a propagating crack to change direction, branch and dissipate energy. Multiply that deflection across hundreds of interfaces and the coating behaves like a composite material that is simultaneously harder and tougher – a combination that single-layer metallurgy cannot deliver.
Nano-scale layering also refines grain growth during deposition. Fine columnar grains pack more densely, leaving fewer pores and coating droplets. This is why premium nano-layer coatings feel smoother to the touch and machine with lower cutting forces in adhesive materials such as low-carbon and austenitic stainless steels, where surface texture of the coating directly influences chip welding behaviour.
Property Comparison: Nano-Layer vs Conventional Coatings
| Property | Monolayer TiAlN (PVD) | Micro-multilayer TiAlN (PVD) | MEGACOAT NANO (PVD) |
|---|---|---|---|
| Typical hardness | 2,800-3,200 HV | 3,000-3,400 HV | approx. 3,300-3,600 HV |
| Oxidation resistance | up to ~800 °C | up to ~900-1,000 °C | up to ~1,100 °C |
| Coating thickness | 2-4 µm | 2-4 µm | 1.5-4 µm |
| Grain structure | coarse columnar | layered, medium grain | nano-refined, dense |
| Edge toughness | good | better | best of the three |
| Best fit | general-purpose work | tough interrupted cuts | high-speed steel machining, BUE-prone materials |
MEGACOAT NANO Grade Portfolio for Steel Machining
Kyocera applies the MEGACOAT NANO principle across dedicated turning and milling grades rather than as a single universal coating. For steel work, three grades cover the large majority of applications:
| Grade | Operation Focus | Typical ISO Range | Character |
|---|---|---|---|
| PR1525 | Steel turning, finishing to medium | P15-P35 | Balanced wear resistance and edge quality for continuous and lightly interrupted cuts |
| PR1535 | Steel turning, medium to rough | P25-P45 | Tougher edge for unstable setups, interruptions and higher feeds |
| PR930 | Indexable milling in steel | P milling | Thermal-cycle resistance for shoulder, face and slot milling |
The family also extends into dedicated grades for stainless steels, cast irons and exotic alloys, so the same nano-layer principle carries across the full application spectrum. When comparing grade data sheets, look at how the substrate hardness and coating thickness are tuned per grade: the nano-layer coating is constant in concept, but the edge preparation and substrate vary by target operation.
How MEGACOAT NANO Attacks the Four Main Wear Modes in Steel
- Crater wear. Driven by diffusion and adhesion on the rake face at high cutting speeds. Smooth, aluminium-rich nano layers resist diffusion and shed chips cleanly, keeping crater growth shallow even at speeds above 300 m/min.
- Flank wear (abrasion). Higher base hardness slows abrasive wear when machining medium-carbon and alloy steels containing hard carbide-forming elements such as chromium and molybdenum.
- Built-up edge. Gummy low-carbon steels weld themselves to the cutting edge at low speeds. A fine-grained, low-friction surface combined with a sharp PVD edge dramatically delays BUE formation – one reason nano-layer PVD has largely displaced uncoated and simple TiN tooling in this field.
- Thermal cracking and edge chipping. Cyclic heating in milling cracks brittle coatings from the outside in. Nano-layer toughness absorbs these cycles, which is why the same coating family covers both continuous turning and interrupted indexable milling.
Recommended Cutting Parameters with MEGACOAT NANO Grades
The values below are practical starting points for coated carbide in rigid setups. Always optimise against actual tool life, and reduce speeds by 20-30% on long tool overhangs, unstable fixturing or older machines.
Turning Steel with PR1525
| Workpiece Material | Typical Hardness | Vc (m/min) | Feed f (mm/rev) | Depth of Cut ap (mm) |
|---|---|---|---|---|
| AISI 1018-1045 low/medium carbon steel | 150-250 HB | 250-350 | 0.15-0.35 | 1.0-3.0 |
| AISI 4140 / 42CrMo4 alloy steel | 250-320 HB | 180-280 | 0.15-0.30 | 1.0-2.5 |
| AISI 8620 / 20MnCr5 case-hardening steel | 170-230 HB | 220-300 | 0.15-0.30 | 1.0-2.5 |
| AISI 12L14 / 1215 free-machining steel | 160-210 HB | 280-380 | 0.20-0.40 | 1.0-3.0 |
- Use the lower half of the feed range when surface finish below Ra 1.0 µm is specified, or switch to a wiper geometry to hold feed rates.
- For interrupted surfaces, step up to PR1535 and reduce Vc by roughly 15-20% to protect the edge.
Milling Steel with PR930
| Operation | Vc (m/min) | Feed fz (mm/tooth) | ap (mm) | ae (% of cutter dia) |
|---|---|---|---|---|
| Shoulder milling, medium steel | 160-240 | 0.10-0.18 | 1.0-4.0 | 50-75 |
| Face milling, roughing | 140-200 | 0.15-0.25 | 2.0-6.0 | 60-80 |
| Finishing passes | 220-280 | 0.06-0.12 | 0.3-1.0 | 30-60 |
- Maintain consistent chip thickness: with light radial engagement strategies, apply the radial chip thinning correction before setting fz, otherwise edge rubbing and chatter will follow.
- PVD grades tolerate flood coolant, but in interrupted milling the thermal cycling between hot cutting and cold flushing can promote cracks. Dry machining or oil mist is often the more stable choice for thin-section parts.
MEGACOAT NANO vs Competing Coating Technologies
Every major tooling group now fields a premium coating answer for steel machining. Comparing the technologies at family level clarifies where MEGACOAT NANO fits:
| Coating System | Technology | Thickness | Key Strengths | Best Suited To |
|---|---|---|---|---|
| Kyocera MEGACOAT NANO | Nano-layer AlTiN PVD | 1.5-4 µm | Balanced hardness, toughness and oxidation resistance | Steel turning and milling, including interrupted cuts |
| Sumitomo ACS | Nano/multilayer AlTiN PVD | 1-4 µm | Similar nano-layer concept, strong AC-series steel grades | Direct competitor in steel turning and milling |
| Sandvik Inveio | Unidirectional CVD alumina | Thicker CVD stack | Exceptional diffusion and crater wear resistance | Stable, continuous steel turning at high temperature |
| Economy monolayer TiAlN | Single-layer PVD | 2-4 µm | Low cost, adequate general performance | General-purpose work at moderate speeds |
Two selection rules follow from this comparison. First, the sharper edge of a PVD coating wins wherever entry shocks exist – milling, interrupted turning, small depths of cut and sticky materials – while thick CVD alumina still rules stable continuous turning at maximum temperatures. Second, within PVD, nano-layer systems outperform monolayer TiAlN in every wear mode that matters in steel; the premium is justified as soon as tool life or surface finish becomes the bottleneck in your process.
Practical Tips for Shop-Floor Success
- Match the grade to the operation. PR1525 for continuous and finishing work, PR1535 where interruptions and vibration dominate, PR930 for indexable milling in steel.
- Respect the minimum speed. Dropping far below the recommended Vc range invites built-up edge in low-carbon steel; it is usually better to reduce feed or depth of cut than to grind along at 120 m/min with a sharp PVD edge.
- Pair coating with geometry. A negative, honed edge suits heavy interrupted cuts; a sharp positive edge suits finishing and stainless work. The coating cannot compensate for the wrong edge preparation.
- Monitor flank wear land. Nano-layer grades typically fail progressively rather than catastrophically, so indexing at 0.25-0.30 mm flank wear protects both the workpiece surface and the remaining edge reserve.
- Know when to leave carbide behind. Above roughly 45 HRC workpiece hardness, move to CBN; for nickel-based high-temperature alloys, ceramic grades become the better answer.
Frequently Asked Questions
Can MEGACOAT NANO grades machine stainless steel?
Yes. The sharp PVD edge and smooth coating resist the built-up edge and notch wear typical of austenitic stainless steels, although Kyocera also offers dedicated stainless grades with optimised edge preparation. Expect starting speeds in the 120-200 m/min range for 304/316 type materials.
Should coolant be used with MEGACOAT NANO?
In turning, flood coolant is acceptable and helps chip evacuation in long-chipping steels. In milling, prefer dry cutting or oil mist to avoid thermal cracking of the edge; if coolant is unavoidable, apply it consistently and continuously rather than intermittently.
How does MEGACOAT NANO relate to the original MEGACOAT?
MEGACOAT NANO is the successor refinement of Kyocera’s original MEGACOAT PVD, shrinking the layer structure from micro-scale to nano-scale. That change delivers higher hardness and oxidation resistance while preserving the edge toughness the original coating was known for.
Conclusion
Nano-layer PVD changed the economics of steel machining by decoupling hardness from toughness. Kyocera MEGACOAT NANO remains one of the benchmark implementations of that idea: start from the parameter tables above, adjust for your rigidity and stability, and let the flank wear land – not catastrophic failure – tell you when to index. For exact grade data on your specific insert geometry, always confirm against Kyocera’s current catalogue figures for the grade and geometry combination you plan to run.
Shop Related Products at HOOGUU